
Ask five mold makers how long a tool takes and you will get five numbers between four weeks and five months. None of them are lies. They are answers to different questions. One is talking about a single-cavity tool in a pre-hardened grade with a cold runner; another is talking about a thirty-two cavity tool with six sliders, a valve gate manifold and a deep grain. The number that decides whether a project succeeds is not the lead time itself — it is whether the schedule behind it survives contact with the two items nobody controls: the steel mill and the manifold supplier.
The short answer, and why it is two numbers
For a normal production tool — single material, no more than two sliders, a standard base, moderate polish — the honest range is eight to twelve weeks from design freeze to first samples. For the same tool to be approved and ready to run production, add four to six weeks. That second number is the one that belongs in a project plan, and it is the one that gets left out of quotations, because it is partly outside the mold maker’s control.
The gap between the two numbers is made of three things. The first is correction: nearly every tool needs at least one round after T1, and many need two. The second is qualification — a dimensional report, a capability study, a first article inspection, whichever the customer’s quality system demands. The third is logistics: crating a tool that weighs more than a small car, booking freight, clearing customs, and getting a press slot at the molder. None of those three are difficult. All three are routinely forgotten, and together they are longer than the machining of the cavity.
So the question “what is your lead time” is not answerable without three more pieces of information: the cavity count, the number of separate moving mechanisms, and whether there is a hot runner. With those three, the range collapses from a factor of five to a factor of one and a half. Any quotation that gives a single figure without asking those questions is a figure that will be revised later, usually by email, usually after the PO.
The number to write into the contract is not the tool lead time. It is: design freeze date, T1 date, the number of correction rounds included, and the date the tool is ready to ship. Four dates. A schedule with fewer than four is not a schedule.
The twelve stages, and which ones are actually on the critical path
A mold is not built by one process that runs from start to finish. It is built by a dozen processes, most of which overlap, and the total time is set by whichever chain of them happens to be longest. That chain is the critical path, and in most tools it does not run through the machine shop. It runs through procurement.
| Stage | Typical working time | On the critical path? | What it actually depends on |
|---|---|---|---|
| Design and DFM review | 3–7 days | Yes, at the start | How complete the 3D and 2D data are, and how many questions come back |
| Mold flow, if it is done at all | 3–5 days | Yes | Whether the gate position is still open, or already fixed by the part |
| Mold base and steel order | 2–6 weeks | Yes — this is the hard start | Standard size from stock, or built to order; which grade, and whether the mill has it |
| Hot runner manifold | 4–8 weeks | Yes, whenever one is used | Stock manifold versus custom; valve gate versus hot tip; the supplier’s own backlog |
| Rough machining | 1–2 weeks | Partly — runs while the base is in transit | Plate size, stock allowance, how many setups the geometry needs |
| Stress relief and hardening | 3–7 days plus queue | Yes, and it resets everything after it | Steel grade; whether the shop has vacuum furnaces in house or sends out |
| Finish machining, wire and sinker EDM | 2–4 weeks | Yes | Number of electrodes; how much fine detail; how tight the tolerance |
| Fitting, spotting and assembly | 1–2 weeks | Yes, and it needs both halves finished | Slider and lifter count; how much spotting is done by hand |
| Texture or polishing | 1–3 weeks | Yes, and it is usually subcontracted | Standard grain or a new pattern; whether mirror polish is specified |
| T1 trial | 1–3 days on the machine | The milestone, not the work | Press time at the molder, not the mold maker’s workshop |
| Correction after T1 | 1–3 weeks per round | Yes | What T1 actually found, and whether it needs new electrodes |
| Dimensional report and qualification | 3–10 days | Yes for regulated parts | Whether a full ISIR or PPAP package is required |
Heat treatment is the stage that resets the clock
Two rows in that table deserve more attention than they usually get. Stress relief and hardening is the stage that resets everything: once a block has been through the furnace, its dimensions have moved, and any finish machining done before it has to be redone or accepted as out of tolerance. Shops that skip stress relief on a large cavity block to save four days usually spend two weeks later machining out a bow that appeared after hardening — and sometimes they do not find it until the tool will not seal. Which grades actually need a furnace trip, and which arrive pre-hardened, is covered in mold steel selection.
Spotting cannot be parallelized
Fitting and spotting is the stage that cannot be overlapped with anything, because it needs both halves of the tool finished. It is also the stage where experience shows most clearly. A tool that has been machined accurately spots in two or three days. A tool that has been machined to a loose tolerance is spotted for two weeks, by hand, with bluing, and the result is still worse. The two weeks saved in the machine shop are paid back with interest at the bench.
The hard start is steel and the manifold, not machining hours
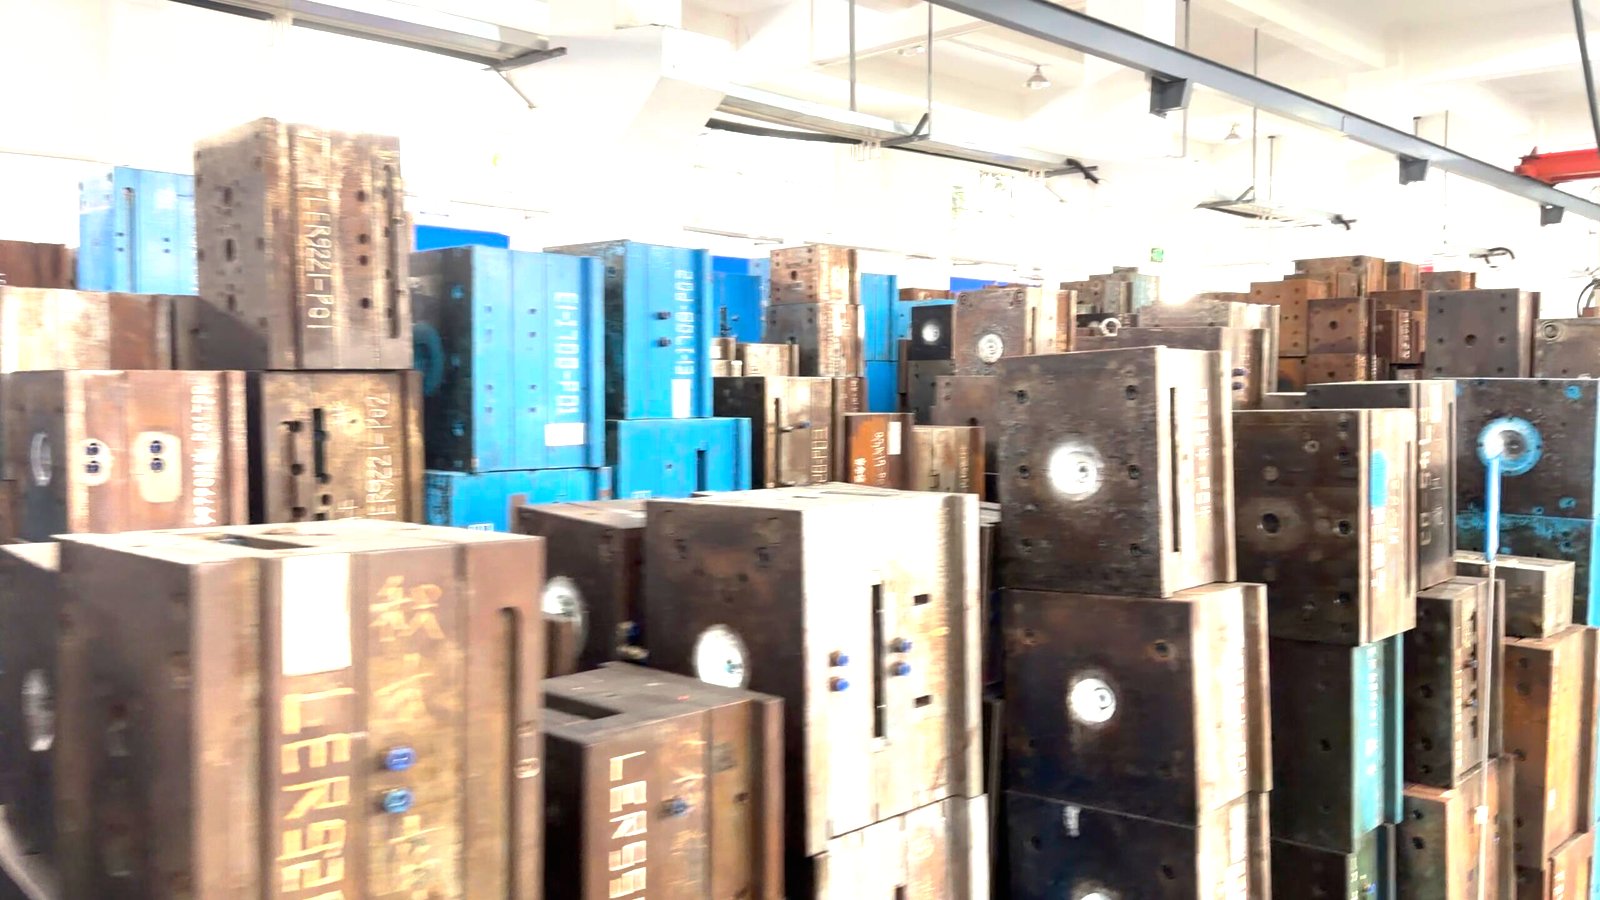
Here is the uncomfortable part of every mold schedule. A workshop can add a second CNC machine, run a night shift, or put three men on the same cavity. A workshop cannot manufacture a hot runner manifold it does not have, and it cannot make a steel mill deliver a block that is not in stock. Those two items sit at the front of the schedule and they are outside the shop’s control, which is why the realistic lead time is so often set before a single chip is cut.
The numbers are worth knowing because they explain the quotes that look impossible. A standard mold base in a common size is typically a two to four week item from a base supplier with stock; a base built to a non-standard size or with unusual pocket positions is four to six weeks. A pre-hardened plate of 718H in a common thickness is often available from stock; the same block in through-hardened H13, or in a stainless grade such as S136 in a large section, may take longer than the base. And a hot runner manifold runs from four weeks for a stock unit to eight or more for a custom layout with sequential valve gates.
This produces a diagnostic that is more useful than any general rule. If a quoted lead time is shorter than the published lead time of the hot runner it specifies, the quote is not describing the same tool. Either the manifold is being taken from someone else’s stock, or it is not included, or the date is aspirational. Asking which manifold, and what its current lead time is, takes one email and settles the question.
The same logic applies to texture. Graining is subcontracted by almost every mold maker, and a grain house with a full calendar is a two to three week item regardless of how fast the tool was machined. Because texture comes after fitting and after any welding, it sits late in the schedule and it has no slack. A tool that is “finished” but not yet textured looks complete in a photo and is still three weeks from T1.
What genuinely cannot be done in parallel
Much of a mold build does overlap, and it is worth knowing which parts, because it explains why two tools of similar size can take very different times. The sequence that turns a drawing into a working tool is described in mold design and mold building; what follows is only the timing of it.
Rough machining runs in parallel with the base order. Inserts and cores can be roughed from bar stock while the base plates are still in transit. This is standard practice and it is where a well-organized shop recovers a week.
Electrodes are made in parallel with the cavity blocks. Electrode blanks are cut and copper is turned while the steel is still being roughed. But the number of electrodes is a direct multiplier on EDM time, and EDM time is not compressible by adding people — one sinker burns one detail at a time.
Fitting cannot start before both halves are finished. This is the real serialization point. Everything upstream can be overlapped; from the moment spotting begins, the tool is one job on one bench.
Heat treatment sits between roughing and finishing, and it is a hard barrier. Nothing can be finished until the block comes back and has been checked. If the block comes back distorted, the schedule gains the time to correct it, and the correction happens at the worst possible moment — after everything else is ready.
T1 depends on a press, not on the mold maker. A finished tool waiting for a trial slot is a common and invisible delay. Trial presses at a molder are booked like any other production resource, and a tool that arrives in a busy week waits. If the schedule matters, the trial date should be booked when the tool is ordered, not when it is finished.
What adds weeks, and what does not
The intuition most buyers have is that time scales with size and cavity count. It does not. Time scales with the number of separate things that have to be made, fitted and proven — and cavity count is one of the cheapest of those.
| Change to the tool | Weeks added | Why it is not linear |
|---|---|---|
| One more slider or lifter | +1 to +2 | Extra machining, extra fitting, extra spotting, and one more mechanism that has to be proven not to jam |
| Two cavities instead of one, same geometry | +0.5 to +1 | The plates and the base barely change; only the cavity set repeats |
| Four cavities instead of two | +0.5 to +1.5 | More electrodes and more EDM hours, plus runner balancing |
| Thirty-two cavities instead of four | +2 to +4 | Base grows two frame sizes, gating has to be balanced by flow analysis, electrode count multiplies |
| Hot runner instead of cold runner | +2 to +5 | The manifold lead time is external and cannot be compressed by working overtime |
| Mirror polish, SPI A-1 | +1 to +2 | Hand work with no shortcut, and it must come after every weld and every correction |
| Deep texture or a new grain | +1 to +3 | Subcontracted; and any later rework means the texture has to be redone |
| Through-hardened H13 instead of pre-hardened 718H | +2 to +3 | Heat treatment, two extra setups, and the risk of distortion that has to be machined out |
| Interchangeable inserts for a family of variants | +1 to +2 per variant | Each variant is fitted and spotted against the same pocket |
| 2K or overmolding | +2 to +4 | Second shot, rotating platen or core-back, two material paths, and adhesion trials |
| Tolerance under ±0.02 mm on several features | +1 to +3 | CMM iteration, and sometimes a second EDM pass after measurement |
| Cavity pressure or temperature sensors | +1 to +2 | Wiring through the tool, controller setup, and tuning before T1 means anything |
| An engineering change after the steel is cut | +1 to +4 each | Re-machining, new electrodes, and occasionally a second heat treatment |
Two entries in that table are worth pulling out, because they run against expectation.
Cavity count is close to free in time
Cavity count is close to free in time, and expensive in everything else. Going from two cavities to four adds perhaps a week: the same electrodes are used, the same base is used, the same fitting procedure is repeated. What it multiplies is the cost of the tool, the tonnage needed, and the cost of every mistake — because a defect that affects one cavity now affects four. Going from four to thirty-two is a different story, because the base grows two frame sizes, the runner has to be balanced with flow analysis, and the electrode count multiplies by eight. The tonnage side of that multiplication is set out in clamp force and tonnage, and the commercial side in what drives mold cost.
Every mechanism costs more than its size suggests
Each additional mechanism costs more than its size suggests. A slider is a set of separate parts — a slide, a heel block, an angle pin, wear plates, a stop, sometimes a spring and a limit switch — and each one has to be machined, fitted, and then proven not to bind when the tool is hot. A single slide typically costs one to two weeks. A lifter is cheaper but has its own failure mode: it must return before the next shot, and if it does not, the tool destroys itself. Five sliders can easily cost more time than a jump from four cavities to sixteen.
The last row of that table is the one that hurts most, because it is the only one caused by the customer. An engineering change after the steel is cut costs more than the weeks it takes. It desynchronizes the electrode queue, it may require re-heat-treatment, and if the change touches a textured surface, the texture has to be stripped and redone. This is why the next section matters more than any other on this page.
The design freeze date is the only date that matters
Every schedule has one date that governs all the others: the moment the geometry stops moving. Before that date, changes are design. After it, changes are rework. The same wall thickness adjustment costs an hour of CAD before the freeze and two weeks of machining after it — and if it happens after heat treatment, it can cost a new block.
This is why a quotation should state the freeze date explicitly, and why a purchase order should too. A schedule that says “twelve weeks” without saying “twelve weeks from design freeze on the 14th” is a schedule with an undefined start, which means it has no end.
There is a practical consequence on the buyer’s side. The window between “we have a 3D model” and “we are ready to freeze” is where most projects lose their schedule, and it is usually lost to work that feels productive: another round of cosmetic review, an unresolved question about the color, a supplier nomination that has not been signed off. None of that is wasted effort. All of it is sequential with the tool, and the tool is the longest item in the project.
Three dates worth writing into the PO explicitly: the design freeze date, the T1 date, and the number of correction rounds included before further rounds become chargeable. The third one is the one that prevents an argument in month four, and it is the one almost nobody writes down.
The freeze also has a technical component that is easy to skip: the DFM review has to happen before the freeze, not after. A draft angle that is too shallow, a wall that is too thin, a boss that will sink — these are cheap to fix on a screen and expensive to fix in steel. A DFM report that arrives after the base has been ordered is a report that will be filed and ignored, because by then the only remaining option is to accept the defect or pay for rework.
T1 is not the finish line
A schedule that ends at T1 is a schedule built by someone who has not run many tools. T1 exists to find out what is wrong. It almost always finds something: a dimension that is out, a weld line in a visible place, a slide that leaves a mark, a short shot at the end of a long flow, a sink on a rib, cooling in one half that is clearly faster than the other. The purpose of the trial is to discover those things while the tool is still in the shop, where fixing them takes days instead of an air freight shipment.
So the realistic plan includes corrections. Two rounds is a reasonable allowance for a mid-complexity tool, and one round is optimistic. Each round has its own internal sequence: measure, decide, machine or weld, refit, re-polish, retest. That sequence is one to three weeks depending on whether new electrodes are needed and whether the surface has to be re-textured.
What T1 should produce is worth being specific about, because a trial that produces only samples produces an argument later. A proper T1 package has four parts:
What a T1 package must contain
Samples from every cavity, marked so that a defect can be traced to the cavity that made it. A process sheet with the actual settings, so the tool can be run again by someone else. A dimensional report against the drawing, with the out-of-tolerance features listed rather than averaged away. And a list of observations from the toolmaker — what was adjusted on the fly, what is marginal, and what they expect to fail first in production.
That last item is the most valuable and the most often missing. The person who spent two weeks fitting the tool knows exactly which slide is tight and which ejector is dragging. If that knowledge is not written down at T1, it is lost, and the molder rediscovers it as a downtime event three months later. What the trial is supposed to establish, and how to sign it off, is set out in mold trial approval.
The weekly evidence you should be asking for
A lead time is a promise about the future, and promises are only as good as the reporting behind them. The difference between a supplier who will hit a date and one who will not is rarely skill; it is whether anyone notices in week four that the tool is three days behind, while three days is still recoverable.
Useful weekly evidence is concrete and cheap to produce:
Five questions every Friday
A photograph of the plates with the job number engraved. This proves the base has physically arrived, which is the single most common invisible delay. The electrode list with a count of what has actually been made, not what is planned. Progress as a percentage against the plan, with the assumption stated — if the shop says 60 percent, ask 60 percent of which stage. A water circuit pressure test record, because a leaking circuit found at fitting is a day and a leaking circuit found at T1 is a week. And the texture booking date, because it is the item that slips without anyone mentioning it.
None of this requires a project management system. It requires a supplier who is willing to be measured, and a buyer who asks the same five questions every Friday. A shop that cannot answer them by Friday is not necessarily dishonest; it may simply not know, which is worse.
Promised lead times that cannot be real
Because lead time is a sales number as much as an engineering one, it is worth knowing which promises are structurally impossible rather than merely optimistic. The same list is a useful part of evaluating a mold supplier, where a schedule that cannot survive scrutiny is usually a sign of other things that will not survive it either.
| What was promised | Why it cannot be true | What to ask instead |
|---|---|---|
| “Tool ready in 4 weeks” on a tool with a hot runner | The manifold alone takes longer than that from most suppliers | Which manifold, and what is its stated lead time today |
| A single number with no design freeze date | The clock cannot start before the geometry stops moving | When does the freeze happen, and what happens if it moves |
| Lead time that excludes texture | Texture is subcontracted and sits on the critical path | Is the grain included, and is the grain house booked |
| Lead time that stops at T1 | Almost no tool is approved at T1 | How many correction rounds are inside the quoted schedule |
| “We will send samples when it is done” | No milestones means no schedule, only an intention | A weekly report with photos, and hold points you can inspect |
| A price that is far below everyone else with the same date | Either the scope is smaller or the date is not real | An itemized scope: what is included, what is extra |
The most common of these is the last one, and it is worth understanding why. Two quotations for the same tool, one far below the other with the same delivery date, usually differ in scope rather than in efficiency. One includes texture, a dimensional report, a spare set of ejector pins, water fittings, a trial at the molder’s site and a correction round. The other includes the tool. Both are honest quotations; they are not quotations for the same thing. The way to find out is to ask for an itemized scope and compare line by line, which takes ten minutes and prevents a very unpleasant conversation in month four.
The second most common is the first row: a date that is shorter than the manifold lead time. This is not always dishonesty — some mold makers hold stock manifolds for common layouts, and a stock manifold genuinely can be a week away. But that is a specific claim, and it can be checked. “Which manifold, and what is its lead time” is a fair question with a factual answer.
How to genuinely compress it
Almost all of the available compression is on the buyer’s side of the table, because almost all of the delay is at the front of the schedule: waiting for a decision, waiting for a freeze, waiting for steel. Paying for overtime in the machine shop recovers days at the end. Deciding faster at the start recovers weeks.
| Action, by whom | Weeks saved | Cost of doing it | Cost of not doing it |
|---|---|---|---|
| Freeze the design before the PO, not after | 1 to 4 | A few more days of engineering before ordering | Every week after steel is cut costs more than the week it takes |
| Let the mold maker order steel against the drawing, before the PO is signed | 1 to 3 | A cancellation risk if the project dies | The project waits for the mill either way, just later |
| Choose a pre-hardened grade such as 718H where the volume allows | 2 to 3 | Lower polishability and a shorter life at high volume | Heat treatment queue plus distortion correction |
| Specify a standard mold base size | 1 to 2 | A slightly larger or heavier base than ideal | A base built to order is a four to six week item |
| Choose a stock hot runner rather than a custom manifold | 2 to 4 | Less freedom in gate position and drop layout | Waiting on a custom manifold with the rest of the tool finished |
| Ship the colorant and the masterbatch with the PO | 1 | Committing to a color before T1 | T1 runs in natural, the color match happens later, and approval is delayed |
| Approve or reject T1 samples within 48 hours | 1 to 2 per round | Someone has to be available | The tool sits finished and idle waiting for a decision |
| Decide the texture before polishing starts | 1 to 2 | Nothing | Polish, then texture, then re-polish after any correction |
| Use a bridge tool in aluminum for launch volumes | 6 to 10 on the first shipment | Shorter tool life, and a second tool later | Missing the launch window entirely |
Three of those deserve a note, because they are counterintuitive.
Ordering steel against the drawing before the PO is signed is the single largest lever available, and it is almost never used. The mill’s lead time is the same either way; the only question is whether it starts before or after the purchasing process finishes. A mold maker who trusts a customer enough to order a base on a handshake is taking a risk, and a customer who wants a short lead time should be willing to accept that the base is billable if the project is cancelled. That is a commercial arrangement, not a technical one, and it is worth a week or two.
Choosing a pre-hardened steel where the volume allows removes the heat treatment queue entirely. Pre-hardened 718H arrives at around 30 HRC and can be machined to final size without a furnace trip, which eliminates both the queue and the distortion risk. It is not right for every tool — it polishes less well than a through-hardened grade and it wears faster in a high-volume tool with abrasive resin — but for a mid-volume tool it removes a two to three week item from the middle of the schedule. The trade-offs between grades are set out in mold steel selection.
Shipping the colorant with the PO sounds trivial and costs a week if it is missed. A T1 run in natural resin tells you about dimensions and filling; it does not tell you about color, and it cannot be used to approve appearance. If the color is decided early, T1 produces approvable parts. If it is decided after T1, the tool waits while a masterbatch is matched.
What no amount of money fixes
What cannot be compressed, at any price, is the sequence inside the steel: rough, relieve, harden, finish, fit, prove. Trying to shorten it by finishing before hardening produces a tool that moves after hardening; trying to shorten it by skipping stress relief produces one that bows. Those shortcuts do not save weeks. They move them.
A schedule you can put in the contract
The table below is a realistic thirteen-week plan for a mid-complexity tool: one material, two to four cavities, two sliders, a standard base, moderate texture. It is a template, not a promise — a thirty-two cavity tool with a valve gate manifold is longer, and a single-cavity tool in a pre-hardened grade is shorter. But it has the right shape, and the shape is what makes it useful: it tells you which week each item should be visible.
| Week | What should be happening | What you should be able to see |
|---|---|---|
| 0 | PO, design freeze, base and steel ordered, hot runner ordered | A signed freeze date. Not “design approved in principle” |
| 1 | DFM report issued, mold flow complete, 3D signed off | The DFM report with the wall thickness and draft findings listed |
| 2–3 | Base arrives, rough machining, electrode design | Photos of the plates with the job number engraved |
| 3 | Stress relief before finish machining | A furnace record or a subcontractor certificate |
| 4 | Hardening, where the grade requires it | Hardness readings, not a promise |
| 5–7 | Finish machining, wire EDM, sinker EDM | An electrode list with the count actually made |
| 6–7 | Texture booked with the grain house | A booking date, because this is the item that slips silently |
| 8–9 | Fitting, spotting, water circuit pressure test | Contact pattern photos and a pressure test record |
| 9 | Hot runner arrives and is installed | Wiring diagram and a heater resistance check |
| 10 | T1 | Samples, a process sheet, and a dimensional report — not just samples |
| 11–12 | Correction, then T2 | A list of what was changed, by cavity number |
| 13 | Final inspection, packing, shipment | Steel certificates, spare parts list, lifting points marked |
Two features of that plan are worth copying into any schedule, whatever the tool. The first is that the hot runner is ordered in week zero, alongside the base, not when the tool is ready for it. The second is that the texture house is booked in week six, before the tool is polished, because a booking is the only thing that reserves capacity. A tool that is polished and waiting for a grain slot has the same delivery date as a tool that has not been polished at all.
What the resulting tool has to achieve at the end of it, in terms of cycle time and consistency, is a separate subject covered in mold cooling design — but the two are connected, because every cooling change after T1 costs a correction round, and every correction round costs a week of the schedule above.
The part nobody schedules: crating, freight and the receiving end
The tool is finished and approved. The project is not delivered. Between those two states sit a crate, a freight booking, a customs declaration, and a press that has to be free when the tool arrives. In practice this stage runs from one week to three months depending on mode, and it is the stage most often left out of the lead time quoted at the start.
| Mode | Transit time | When it is the right choice | What people forget |
|---|---|---|---|
| Air freight | 5–10 days door to door | A tool under about 500 kg, or a schedule that has already slipped | Cost scales with volume weight, and a crated mold is mostly air |
| Sea LCL | 25–40 days port to port | The normal case for a production tool | Add two weeks for crating, inland haulage and customs at both ends |
| Sea FCL | 22–35 days | Several tools shipping together | The container has to be booked, and a 3 t mold needs a certified lifting frame |
| Rail to inland Europe | 18–25 days | When the destination is inland and the sea port adds a week of trucking | Route and schedule are less flexible than sea |
Three practical details are worth settling before the tool ships, because each of them can stop a project at the receiving end with the tool already paid for.
Three details to settle before the tool leaves
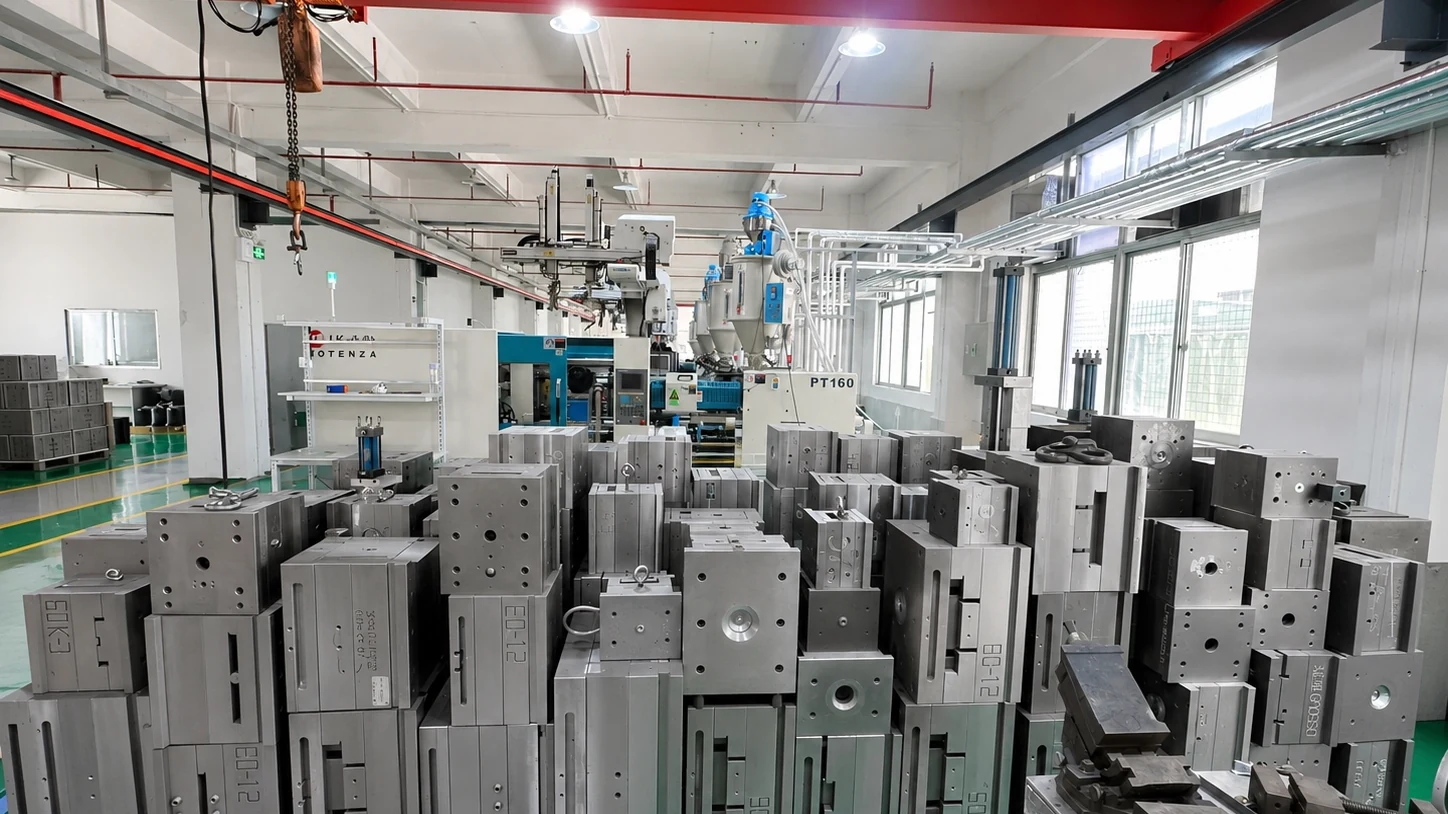
The lifting points and the crate. A production mold can weigh several tonnes, and it must be lifted from designated lifting holes, not from the parting line or from an eyebolt screwed into a water fitting. The crate needs a base that can take the point load and skids that a forklift can reach. A mold that arrives in a crate with no marked lifting points is a mold that gets lifted wrongly at the molder, and the damage is usually to the ejection system.
The water fittings and the spare parts. Every circuit should arrive with its fittings installed or bagged and labeled, with a circuit diagram that matches the actual plumbing. The spare parts list matters more than it looks: ejector pins, springs, a spare slide wear plate, and the seal kit for any hydraulic cylinder. A worn ejector pin is a two-day delay if a spare is in the crate and a three-week delay if it has to be shipped.
The press slot at the molder. The receiving factory has to have the machine free, the crane available, the dryer and chiller connected, and the resin in stock. All four are someone else’s schedule. A tool that arrives on time into a factory that is not ready is a tool that has not been delivered, and the delay is often attributed to the mold maker because the tool is the visible item.
One more, specific to regulated parts: if the part needs a first article inspection or a capability study at the molder, that work happens after the tool arrives, on the molder’s machine, with the molder’s operators. It takes days to weeks, it cannot be done in advance, and it belongs in the project schedule from the beginning. For a tightly toleranced part it is often the longest single item after T1.
None of this is exotic, and none of it requires a new system. It requires the schedule to include the whole journey rather than the interesting part of it. If you are comparing dates against a launch plan and want a second opinion on whether a schedule is realistic, send us the part drawing and the target date — the answer depends far more on the cavity count, the mechanism count and the steel grade than on anything else, and it can usually be given in a day.
Frequently asked questions
How long does it take to make an injection mold?
Eight to twelve weeks from design freeze to first samples for a normal production tool, and twelve to sixteen weeks to have it approved and running. The lower end applies to a single-cavity tool in a pre-hardened grade with a cold runner and a simple polish. The upper end applies to anything with a hot runner, multiple sliders, deep texture or a regulated part that needs a full qualification package. The variation between those two cases is larger than the variation between competent suppliers, so the specification matters more than the shop when comparing quotes.
Can I pay more to get it faster?
Partly. Money can buy night shifts, extra machine time, air freight instead of sea, and a stock manifold instead of a custom one. It cannot buy steel that is not in the mill’s stock, a grain slot that is not available, or time for heat treatment to complete. The realistic effect of paying for acceleration is a ten to twenty percent reduction, concentrated in the machining and fitting stages. Anyone promising to halve a lead time is either moving work outside the scope or planning to skip a step that will be paid for later — most often stress relief, which shows up as a tool that will not seal after hardening.
Does adding cavities increase lead time?
Much less than people expect. Going from two cavities to four adds roughly half a week to a week: the base and plates are the same, the fitting procedure is repeated, and the same electrodes are used. The cost multiplies far more than the time. The jump that does add time is four to thirty-two, where the base grows two frame sizes, the runner has to be balanced by flow analysis, and the electrode count multiplies. As a rule, add a week per doubling of cavities up to eight, then budget two to four weeks for a large multi-cavity tool on top of that.
How long does a hot runner add?
Two to five weeks, and almost all of it is the manifold supplier’s lead time rather than any work in the mold shop. A stock manifold for a common layout can be a week away; a custom manifold with sequential valve gates is more often six to eight weeks. Because the manifold sits at the front of the schedule but is installed late, a late manifold stops a tool that is otherwise finished. This is why it should be specified and ordered at the same time as the mold base, and why the question “which manifold and what is its current lead time” is worth asking before signing.
How long does a correction after T1 take?
One to three weeks per round. The sequence is fixed: measure the samples, decide what to change, machine or weld, refit, re-polish, retest. The variables are whether new electrodes are needed, which adds several days, and whether the change touches a textured surface, which means stripping and re-graining. A change to a core insert that can be re-machined from the existing electrode is the fast case. A change to a cavity surface that has already been grained is the slow case, and it is the reason texture should be specified early and applied late.
Can I get parts before the production tool is finished?
Yes, and it is a reasonable thing to plan for. Two routes exist. An aluminum bridge tool can typically produce a launch quantity in four to six weeks, which is six to ten weeks ahead of a hardened production tool, at the cost of a shorter tool life and a second tool later. Alternatively, a low-volume aluminum tool may be enough for the whole program if volumes are small. What does not work is asking the production tool to arrive early and also be correct; the two requests pull in opposite directions, and the tools that arrive early are the ones with the most correction rounds after them.
What is the difference between tool lead time and project lead time?
Tool lead time ends when samples are approved. Project lead time ends when parts are in the warehouse. Between them sit the qualification package, the packing and crating, the freight, the customs clearance, the receiving factory’s readiness, and the first production run at rate. On a sea shipment to Europe or North America that gap is commonly six to ten weeks, which is longer than the correction rounds and is routinely left out of the plan. A project schedule that shows the tool arriving on the required date has not answered the question of whether parts will be available on that date.
Why do two suppliers quote lead times three weeks apart for the same tool?
Usually because the scope differs, not the speed. One quotation may exclude texture, exclude the dimensional report, exclude the trial at the customer’s molder, and include only one correction round. Another may include all four and a spare parts kit. Three weeks is a realistic difference between those two scopes. The other common cause is the starting point: one supplier is counting from the PO date, the other from a design freeze that has not happened yet, and the gap between those two dates is often three weeks of the customer’s own engineering review. Ask what the start date is and what is included, and the two quotes usually converge.