Mold Ejection System: Why Parts Stick and How to Fix It
Shrinkage grip, draft angle and pin layout, plus the alternatives when pins are wrong, and why parts stick even with generous draft.
Shrinkage grip, draft angle and pin layout, plus the alternatives when pins are wrong, and why parts stick even with generous draft.
What fill, packing, cooling and warpage analysis each answer, where the error comes from, and how to check the prediction against the trial.
Choose a resin from service temperature, chemical exposure and tool consequences rather than price per kilo, with shrinkage, drying and steel tables.
Vent depth by resin, where to cut the lands, why trapped air burns, and how to tell a venting fault from a process fault.

How to set cavity count from volume, peak demand, press size and tool payback, and why runner balance decides whether a multi-cavity tool really runs.
Why injection mold lead time is set by the steel mill and the manifold supplier rather than machining hours, and what actually compresses it.
How to calculate clamp force from projected area and cavity pressure, why the nameplate figure is wrong, and what over-clamping does to a tool.
Why cooling sets 60 to 70 percent of the cycle, what turbulence and channel distance actually do, and how to spot a tool problem.
The twelve design decisions that decide what a mold costs, ordered by how expensive each one becomes once the steel is cut.
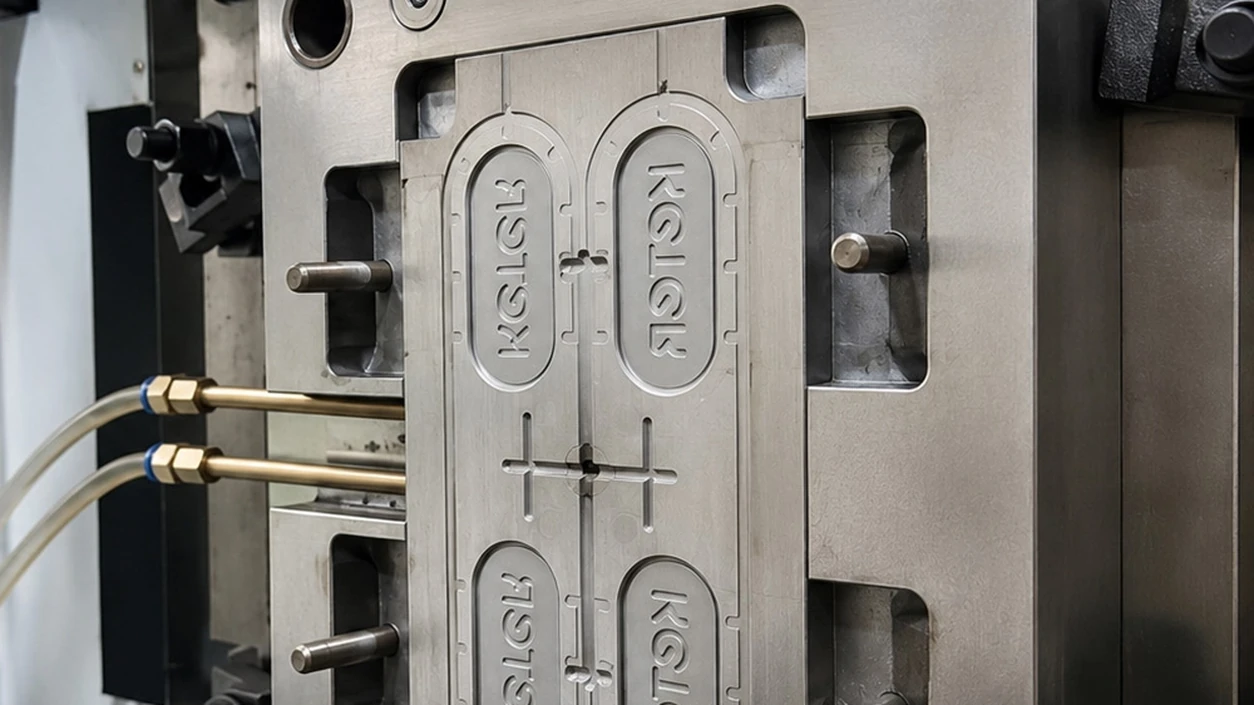
What a mold can really hold, why shrinkage rather than machining sets the limit, what each tolerance step costs, and how to specify finish.